Logo for Australian Made and Owned certification

Safety Barriers For Storage Facilities

Storage facilities are built for density. High-bay racking, narrow aisles, mezzanine floors, and compact loading areas are all designed to maximise the use of every square metre. That density creates a real safety risk when forklifts, trucks, and workers on foot share the same tight spaces across every shift.

Verge Safety Barriers works with storage facility operators across Australia to put the right physical controls in place. Protecting workers from vehicle movement, protecting racking and infrastructure from forklift impact, and helping operators meet their WHS obligations across every zone in the facility.

WHY STORAGE FACILITIES NEED SAFETY BARRIERS

Density And Hazard Go Hand In Hand

The same design features that make a storage facility efficient also make it hazardous. Narrow aisles give forklifts limited clearance around racking uprights. High-bay storage creates falling object risks from every elevated level. Compact loading areas bring trucks and forklifts together in confined spaces. And the workers who operate in these environments do so at close proximity to moving vehicles for most of their shift.

Australian WHS legislation requires operators to identify and control these hazards at the highest reasonably practicable level. For storage facilities, that means physical separation between pedestrian and vehicle zones, protection for racking and structural elements from forklift impact, and compliant edge protection at every elevated work area.

The cost of not acting is high. A racking collapse triggered by an unprotected upright impact can cause serious injury, destroy stock, and take a facility offline for weeks. A forklift and pedestrian collision in an unguarded aisle is a notifiable incident under WHS legislation. Physical barriers address these risks permanently and documentably.

ULD Storage solution​

KEY STORAGE FACILITY SAFETY ZONES

Where Verge Products Make The Biggest Impact

Racking Aisles and End-Of-Aisle Protection

Racking end frames are the most frequently damaged structural element in any storage facility. Rack-PRO end-of-aisle protectors absorb forklift impacts before they reach the upright, preventing the cumulative damage that leads to racking failure. In narrow aisle environments, low-profile protection that does not restrict forklift clearance is essential.

Pedestrian Walkways and Traffic Lane Separation

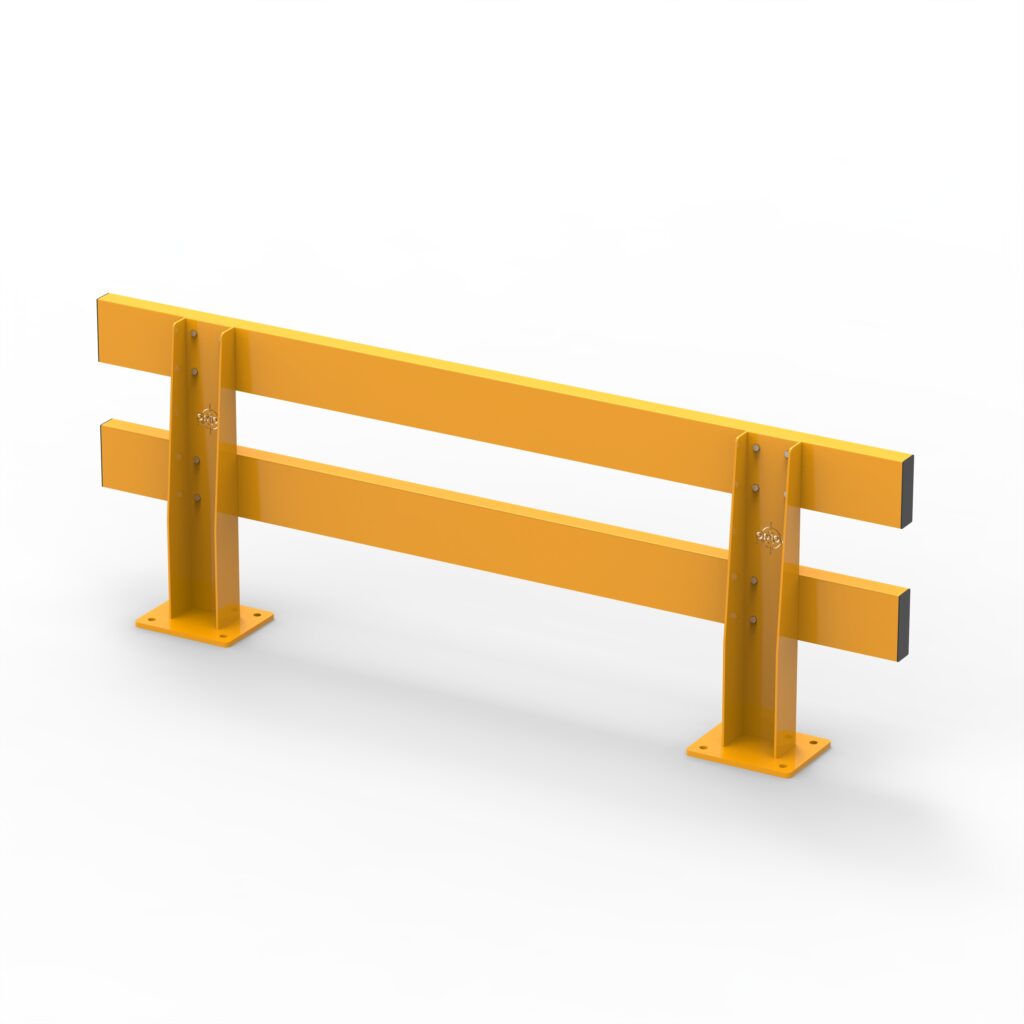
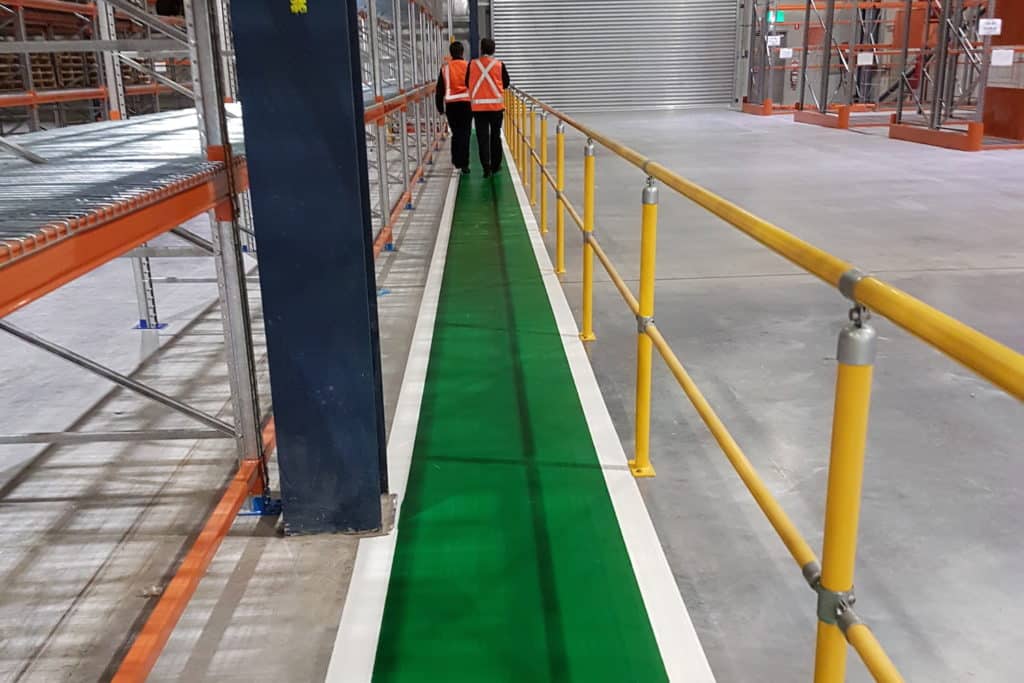
Where workers on foot need to move through or alongside forklift operating areas, physical separation is the only reliable control. HD Barriers and ECO-Rail create defined pedestrian laneways that keep workers out of the forklift path, including at the aisle entry and exit points where the collision risk is highest.

Loading and Receiving Areas

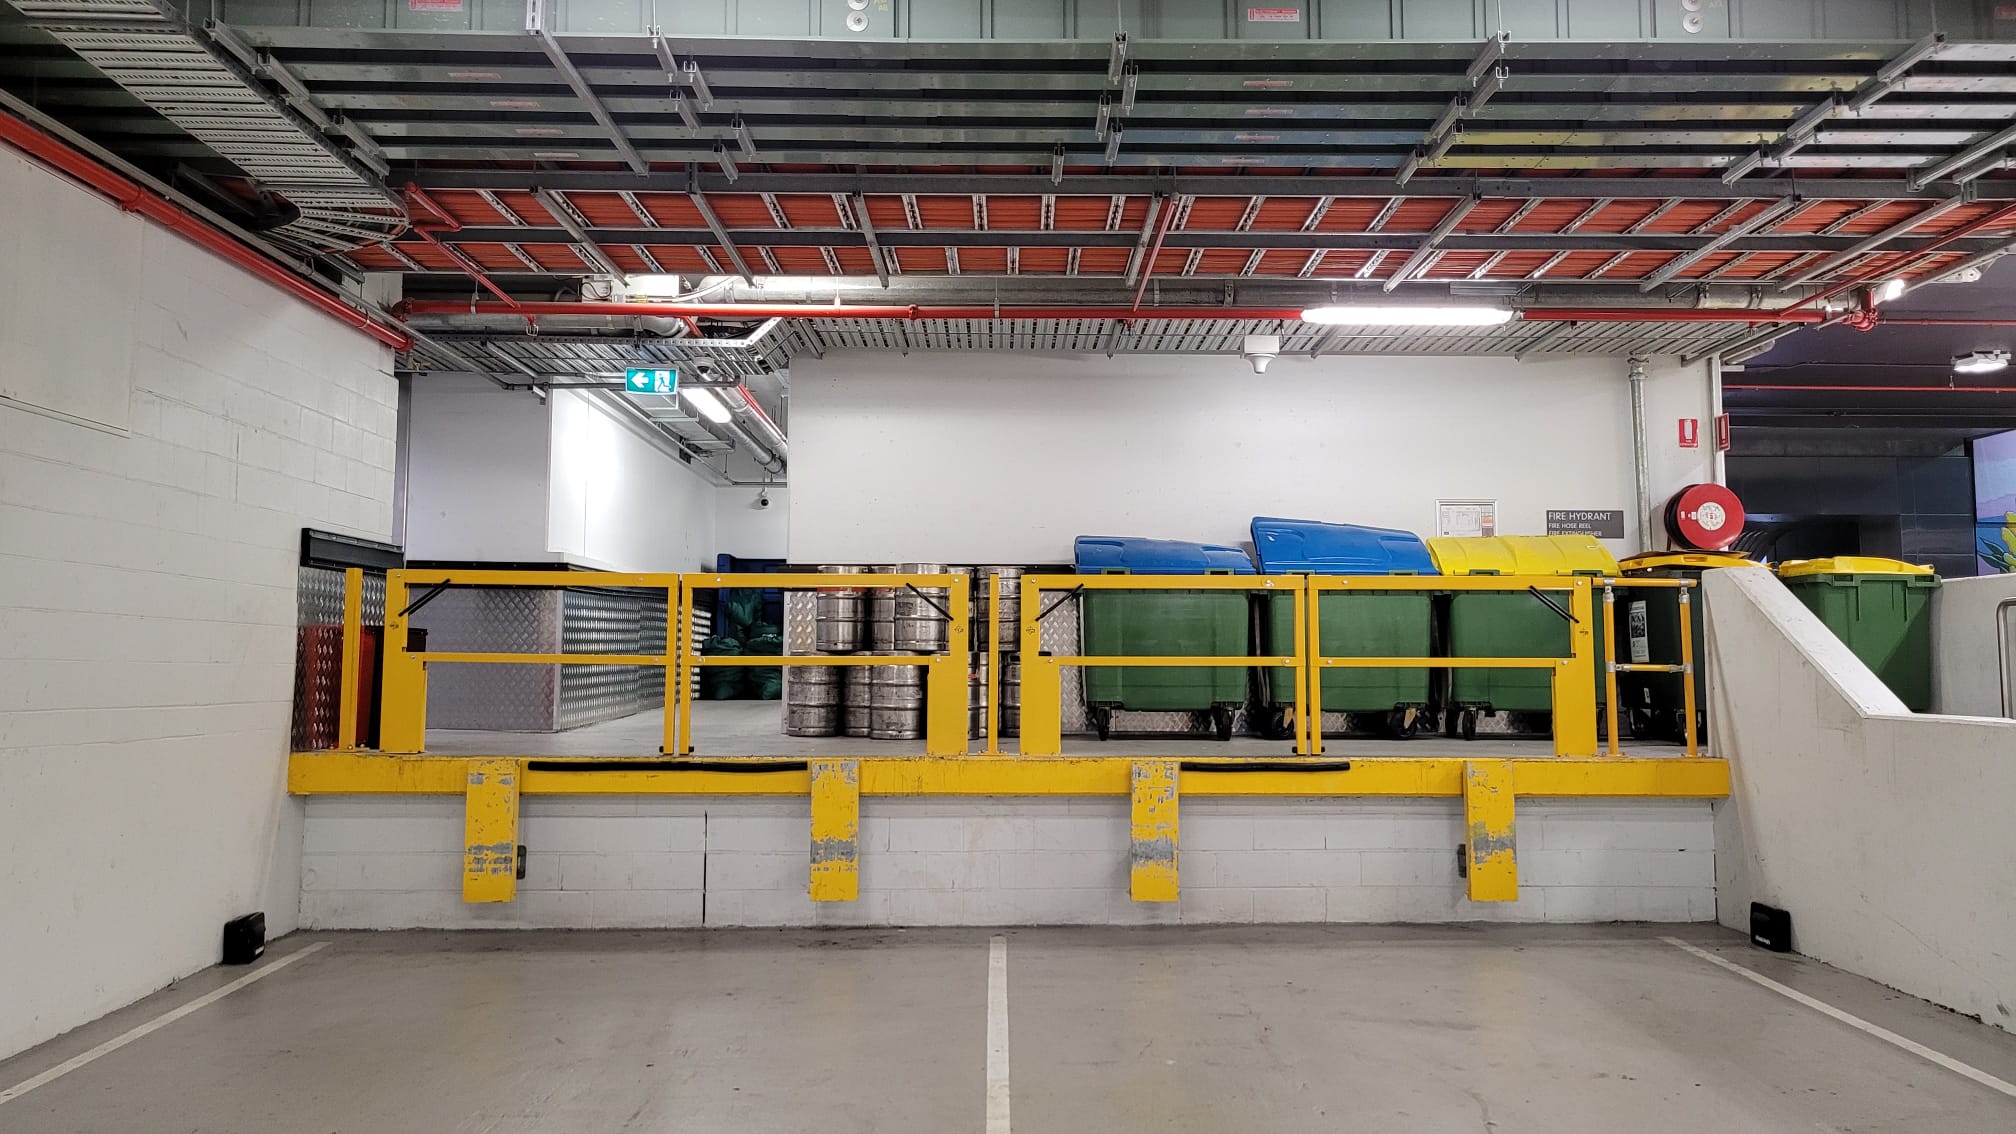
The receiving area of a storage facility is where delivery vehicles, forklifts, and dock workers converge. Dock-PRO gates provide edge protection at open dock faces, while barriers and bollards define safe zones around receiving and staging areas to keep pedestrian and vehicle movements separated during inbound operations.

Mezzanine Floors and Elevated Storage Areas

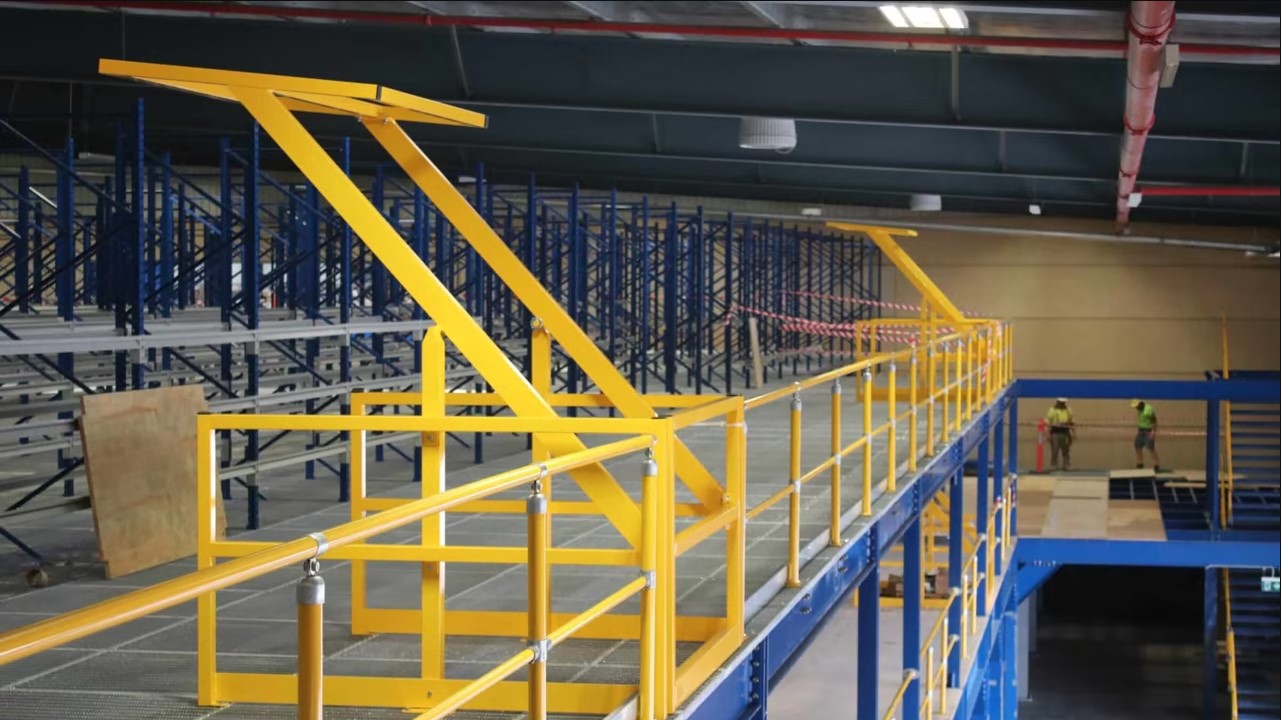
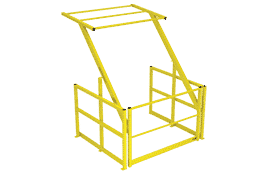
Storage facilities frequently use mezzanine floors to maximise vertical space. Open edges, pallet transfer points, and stairwell entries on mezzanine floors require compliant edge protection, rollover pallet gates, and guarded access points to meet Australian fall prevention requirements.

Column and Wall Protection

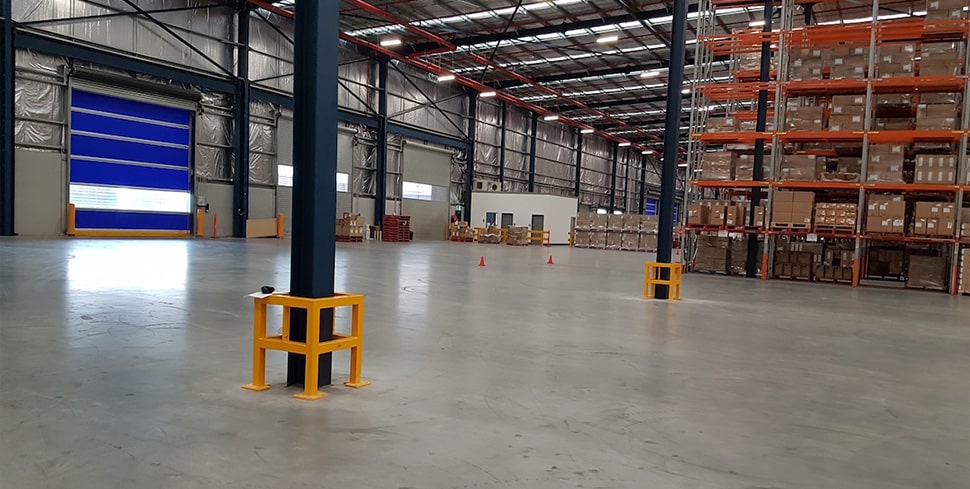
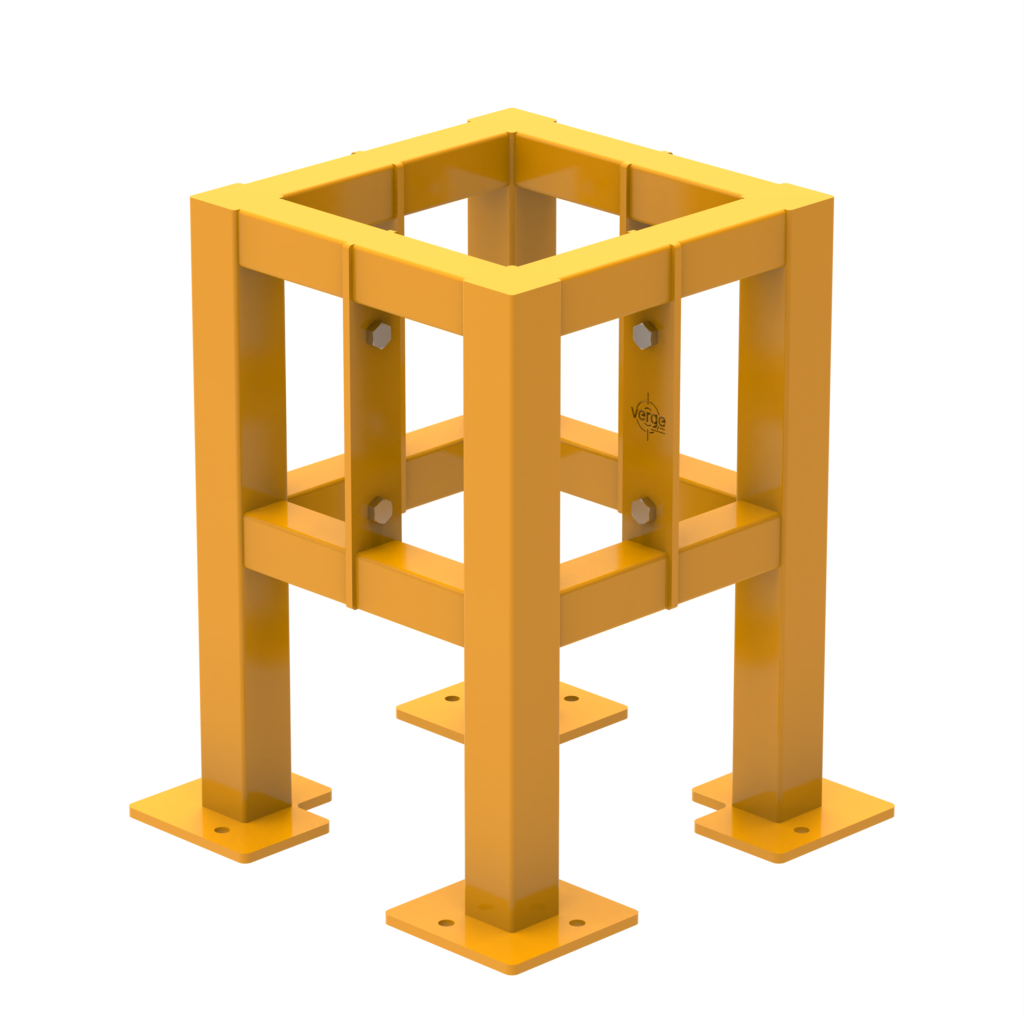
Structural columns throughout the storage facility are vulnerable to repeated forklift contact in high-density environments. Column protectors wrap the column and absorb impact energy before it reaches the steel, reducing the risk of structural damage that can affect the integrity of the racking system or the building itself.

Overhead Door and Entry Protection

Roller doors and overhead door frames at facility entries and internal doorways take constant impact from forklifts and reach trucks passing through. Overhead door protectors and door frame guards prevent this damage from accumulating to the point where doors fail or require costly replacement.

Racking Aisles and End-Of-Aisle Protection Pedestrian Walkways and Traffic Lane Separation Loading and Receiving Areas Mezzanine Floors and Elevated Storage Areas Column and Wall Protection Overhead Door and Entry Protection

CASE STUDIES

Trusted By Australian Storage Facility Operators

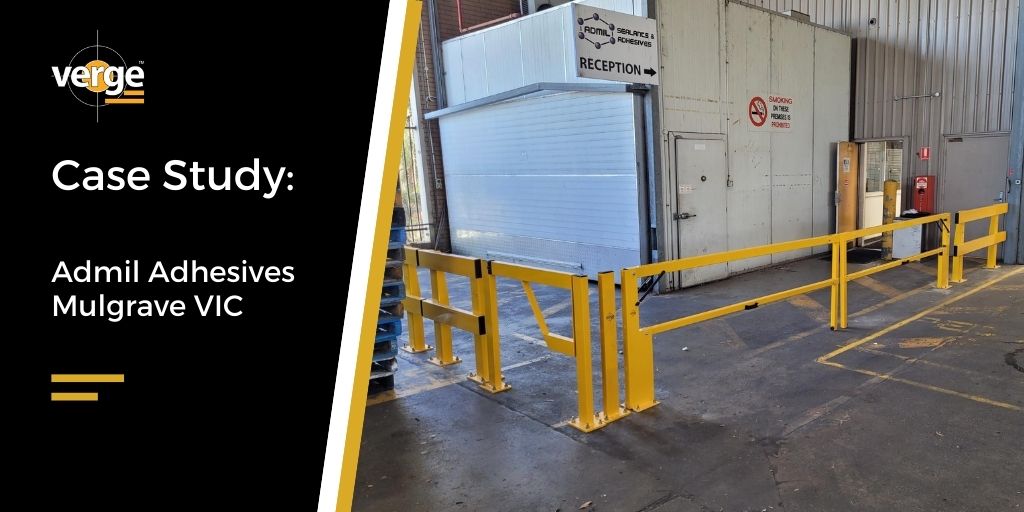
Admil Adhesives Mulgrave VIC

Admil Adhesives undertook a site safety upgrade as their production floor team grew and painted line demarcation was no longer considered an acceptable means of separation. The safety team selected the Australian-made HD Barrier as their chosen barrier system, and Verge completed the comprehensive upgrade across the Mulgrave facility to provide physical pedestrian segregation and forklift traffic management.

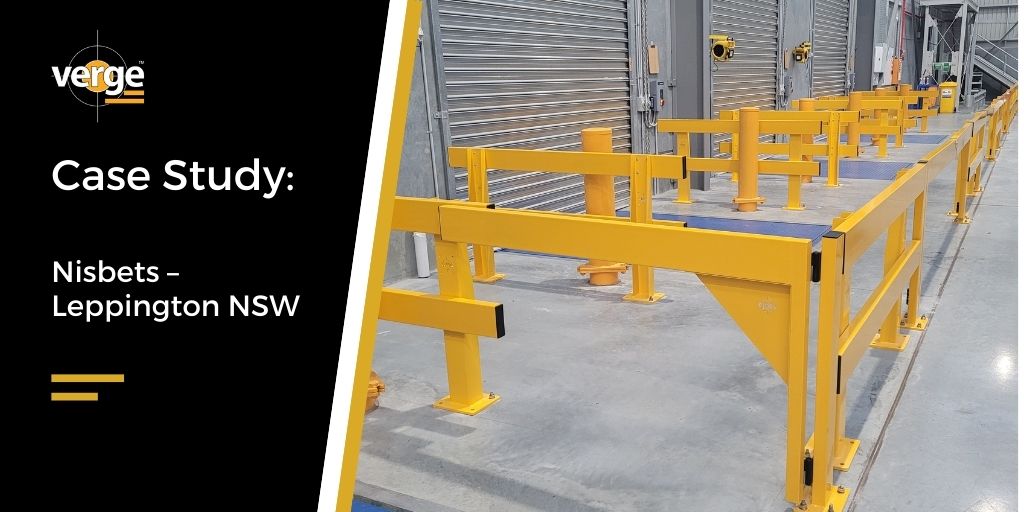
Nisbets – Leppington NSW

Nisbets moved into a new factory with minimal HD Barrier already on site and a number of unprotected areas exposed to forklift traffic, including an open dock area. Verge proposed additional barriers, boom gates for dock access points and column protectors at locations where forklifts operated near unprotected structural columns. This was Nisbets’ second facility protected with Verge solutions, reflecting their proactive approach to safety. Designated walkways and controlled intersections removed the uncertainty for both pedestrians and forklift operators across the site.

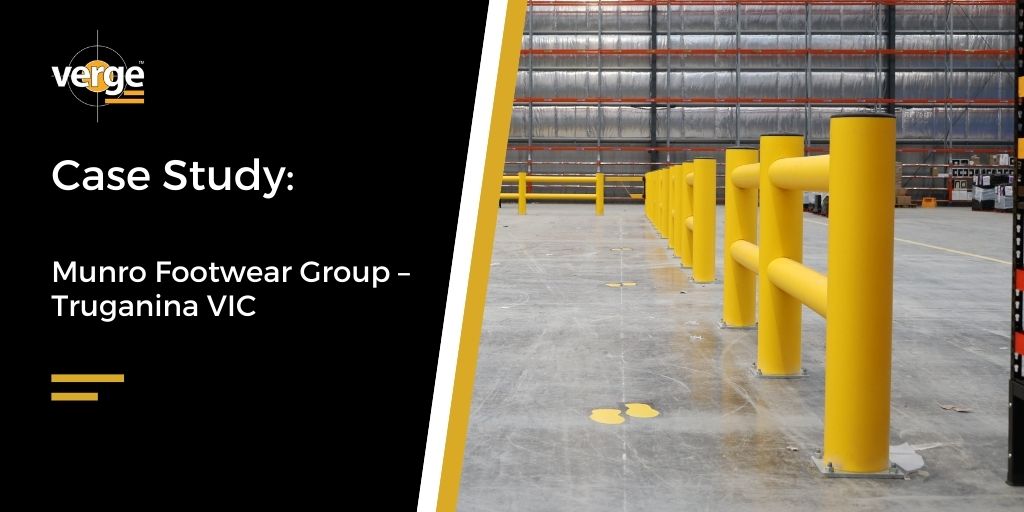
Munro Footwear Group – Truganina VIC

Munro Footwear Group invested in a new distribution centre with full automation and needed a safety barrier partner to protect their warehouse team from forklift traffic. Verge was engaged by Qanstruct Australia to supply and install the full barrier package. Munro chose the Impact HDP Barrier as an Australian-made product to safely segregate forklift and pedestrian traffic. The installation was completed prior to Practical Completion so Munro could begin operations immediately.

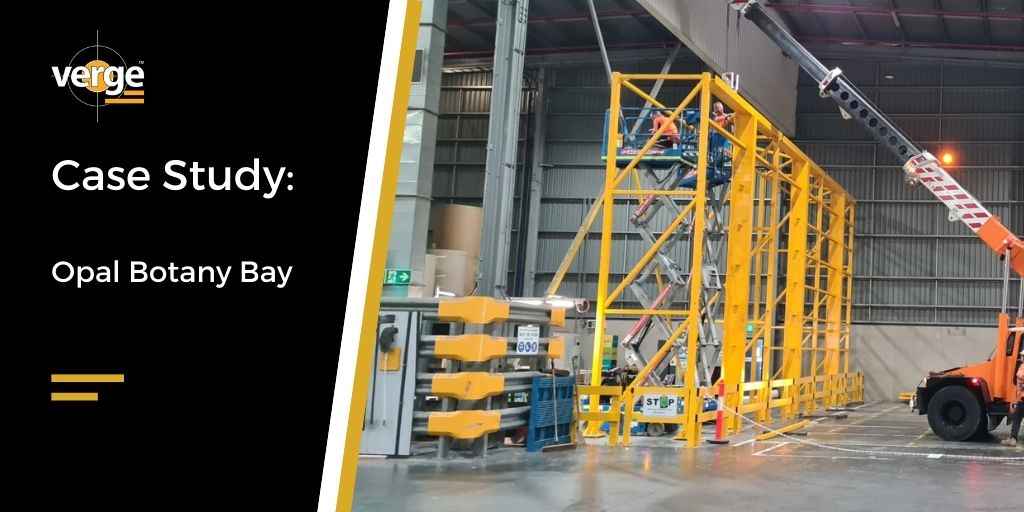
Opal Botany Bay

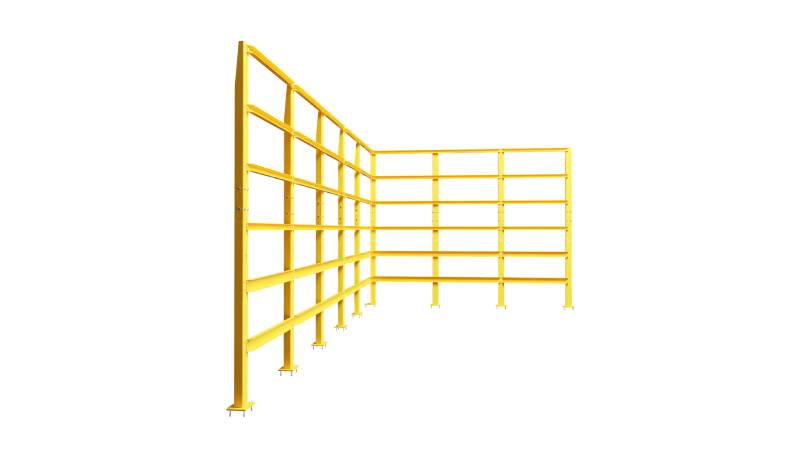
Opal’s warehouse stored bulk paper rolls weighing up to 3,500 kg, stacked three and four levels high in an area adjacent to a truck driver safe zone. The risk of a roll toppling into the driver zone created a potential crush injury hazard. After evaluating options including reducing stack heights (which would have cost valuable warehouse capacity), Verge designed and constructed a 7-metre high topple barrier 14.5 metres long using the Hy-Wall system. The structure was erected in 1.5 days with minimal disruption. Both the warehouse capacity and driver safety zone were preserved.

WHY CHOOSE VERGE FOR STORAGE FACILITY SAFETY

Australian Made, Storage Ready

Australian Made and Owned

Every Verge product is manufactured at our Glendenning, NSW facility, meaning faster delivery, local technical support, and products designed specifically for Australian conditions and WHS compliance requirements.

Racking Protection Expertise

Protecting racking from forklift impact is one of the most critical safety and asset protection priorities in any storage facility. Verge Rack-PRO systems are designed specifically for this application, providing effective end-of-aisle protection without restricting forklift access or reducing aisle clearance.

WHS Compliant

Verge products are designed to meet Australian Work Health and Safety standards, helping storage facility managers document their hazard controls and demonstrate duty of care to regulators, insurers, and auditors.

Handles High-Density Environments

Storage facilities put safety infrastructure under constant load in tight spaces. Verge barriers and protection products are engineered to handle repeated forklift contact without failing, so your safety controls remain effective regardless of how busy the facility gets.

Modular And Relocatable

Storage layouts change as stock profiles, client requirements, and racking configurations evolve. Verge's modular product range can be reconfigured, relocated, or extended as your facility changes, without replacing existing infrastructure.

Fast Lead Times

Local manufacturing means we can respond quickly when a safety gap needs to be addressed, without waiting on international supply chains or extended lead times.

Protect your Storage Facility with Verge Safety Barriers

Every storage facility has a different layout, racking configuration, and operational pattern. Whether you need to protect racking from impact, separate pedestrians from forklifts, or secure a mezzanine edge, Verge can help you find the right solution.

Contact us today for a free site assessment and quote.

$100 Verge gift voucher stack image

Receive A $100 Gift Voucher

SIGN UP TO OUR NEWSLETTER TO RECEIVE YOURS TODAY

*Applies to online orders only. *Cannot be used in conjunction with any other offer  **Must purchase within 3 months of receiving the voucher  ***Minimum order $1000

"*" indicates required fields

This field is for validation purposes and should be left unchanged.
Your Industry*

WAIT!

Before you go, check out this video.

If you need assistance with selecting a product, would like a quote or want to ask a question please call our friendly team on 1800 765 539

Download Brochure

  • This field is for validation purposes and should be left unchanged.