Logo for Australian Made and Owned certification

Safety Barriers For Meat Packing Facilities

Meat packing and processing facilities are among the most demanding industrial environments in Australia. They combine heavy forklift and vehicle traffic with strict food safety standards, constant washdown regimes, and cold, wet working conditions that are tough on people, equipment, and infrastructure alike.

Verge Safety Barriers works with meat processors and packing facilities across Australia to put the right physical controls in place. Separating workers from forklifts, protecting equipment and infrastructure, and providing safety barriers that withstand the corrosive, high-hygiene, temperature-controlled conditions of a meat processing environment.

WHY MEAT PACKING FACILITIES NEED SAFETY BARRIERS

A Harsh Environment with High Stakes

Meat processing facilities present a combination of hazards rarely found together anywhere else. The floors are wet and frequently slippery. The environment is cold, often at or below freezing in storage areas. Forklifts move carcasses, product, and packaging continuously. Workers operate on foot across processing floors, boning rooms, packing areas, and chillers throughout their shift. And the entire facility is subject to daily high-pressure washdown and sanitation.

This environment is brutal on standard safety infrastructure. Corrosion from washdown chemicals, the constant temperature variation between chillers and processing floors, and the relentless forklift traffic all combine to destroy barriers that are not built for the conditions.

Australian WHS legislation requires meat processors to control forklift and pedestrian hazards with effective physical measures, and food safety standards require that all surfaces in the facility can be cleaned to a hygienic standard. Verge products are manufactured to meet both requirements in an environment that punishes anything less.

verge safety barriers meat packing

KEY MEAT PACKING SAFETY ZONES

Where Verge Products Make the Biggest Impact

Processing and Boning Room Floors

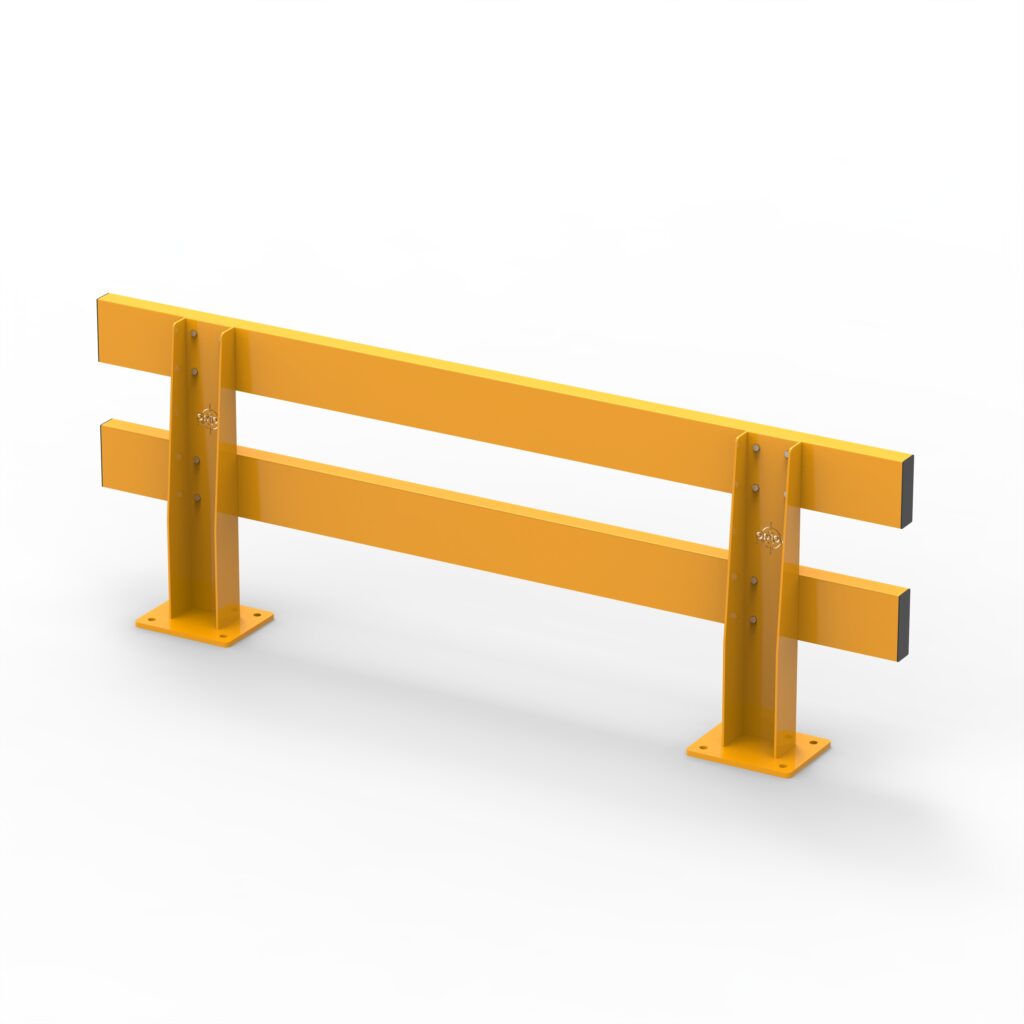
Processing and boning rooms combine wet, slippery floors with workers on foot and forklifts moving product through the area. HD Barriers and ECO-Rail create defined separation between the forklift path and the pedestrian work zones, protecting workers who are focused on the task in a high-activity environment.

Chillers and Freezer Storage Areas

Chiller and freezer entries are high-traffic, low-temperature pinch points where forklifts and workers cross constantly. Overhead door protectors prevent damage to door seals and frames that are critical for temperature control, while column protectors and barriers absorb forklift impact in these confined, high-use entries.

Packing and Carton Handling Areas

The packing area sees finished product cartoned, palletised, and prepared for dispatch, with forklifts moving completed pallets through the zone. Barriers define safe zones around packing lines and palletising equipment, keeping workers separated from forklift traffic during the high-volume packing process.

Loading Docks and Dispatch Areas

The dispatch dock at a meat facility handles refrigerated transport loading under tight temperature and time controls. Dock-PRO gates provide edge protection at open dock faces, while barriers and bollards define safe zones around the dispatch area and keep workers separated from reversing trucks and forklift movement.

Hygiene Control and Gowning Areas

The transition points between hygiene zones, including boot wash, gowning, and sanitation control points, require defined pedestrian routing that maintains both worker safety and food safety compliance. Barriers and rail systems guide foot traffic through the correct control points while keeping workers clear of vehicle movement.

Column and Equipment Protection

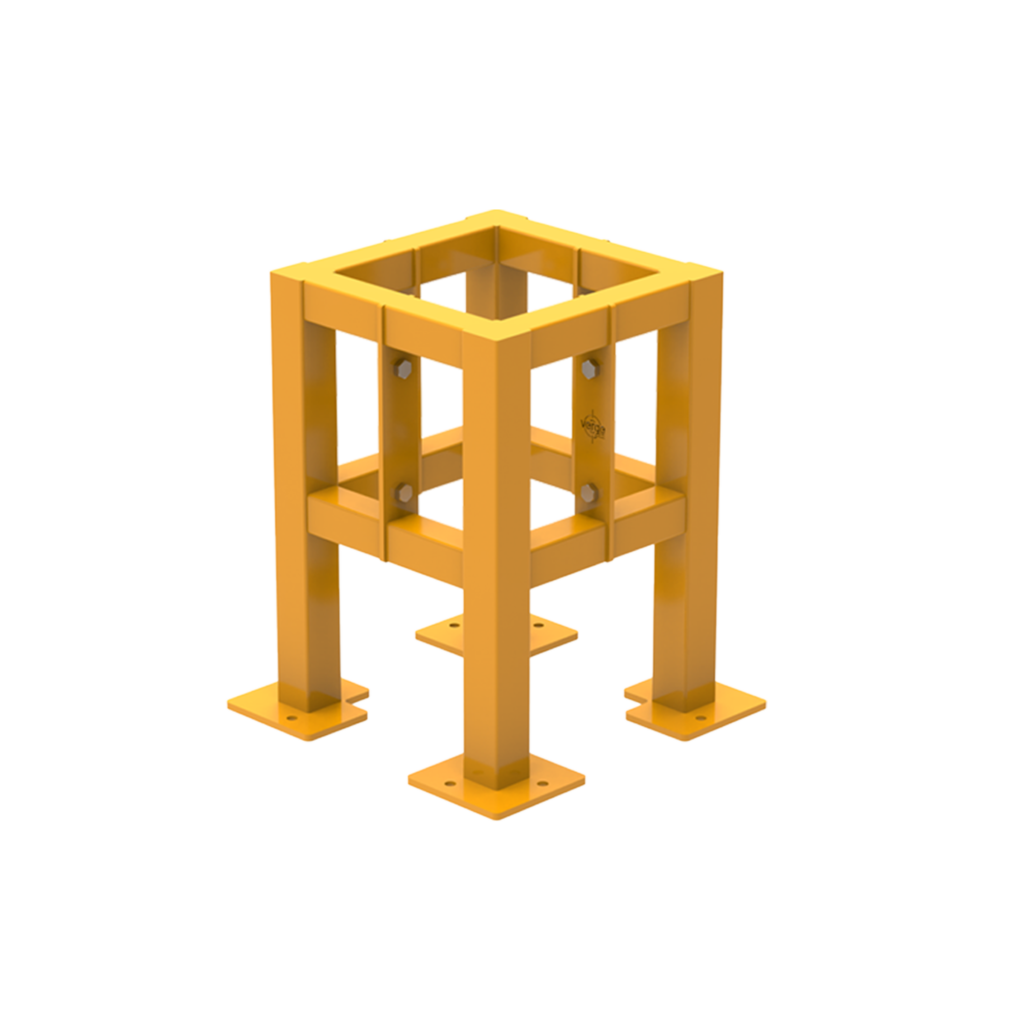
Structural columns and fixed processing equipment are vulnerable to repeated forklift contact in the tight, high-traffic spaces of a meat facility. Column protectors and equipment guards absorb impact before it reaches the structure or machinery, protecting both the asset and the production continuity that depends on it.

Processing and Boning Room Floors Chillers and Freezer Storage Areas Packing and Carton Handling Areas Loading Docks and Dispatch Areas Hygiene Control and Gowning Areas Column and Equipment Protection

RECOMMENDED PRODUCTS FOR MEAT PACKING FACILITIES

CASE STUDIES

Trusted By Australian Food And Processing Operators

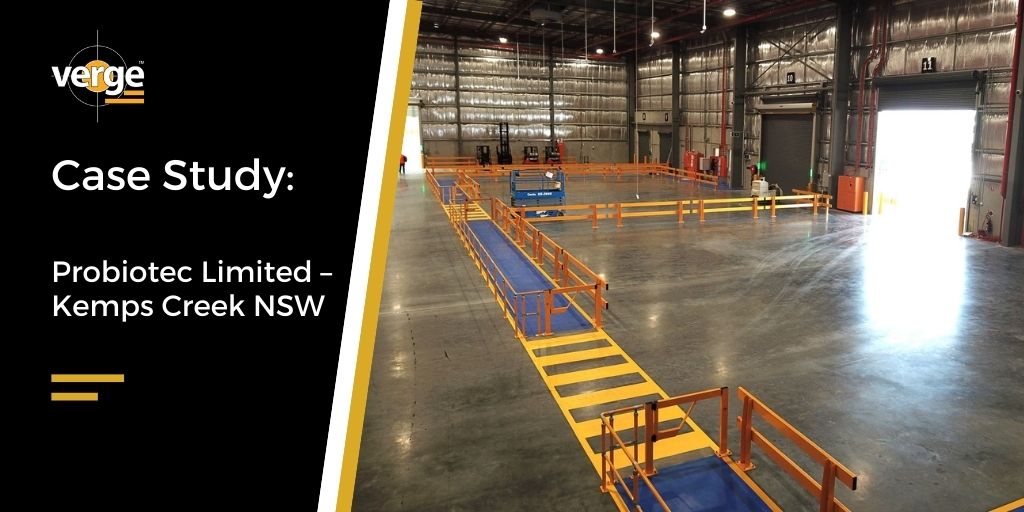
Probiotec Limited – Kemps Creek NSW

Verge supplied and installed over 1,000 metres of safety barriers, gates and related products at the Probiotec Limited pharmaceutical facility in Kemps Creek, working with Mainbrace Constructions in a tight timeframe with precise coordination required throughout. The project demanded proactive problem-solving and open communication to stay on schedule. The client feedback on completion was described as ‘just UNREAL, just PERFECT,’ reflecting the standard of workmanship and project management delivered.

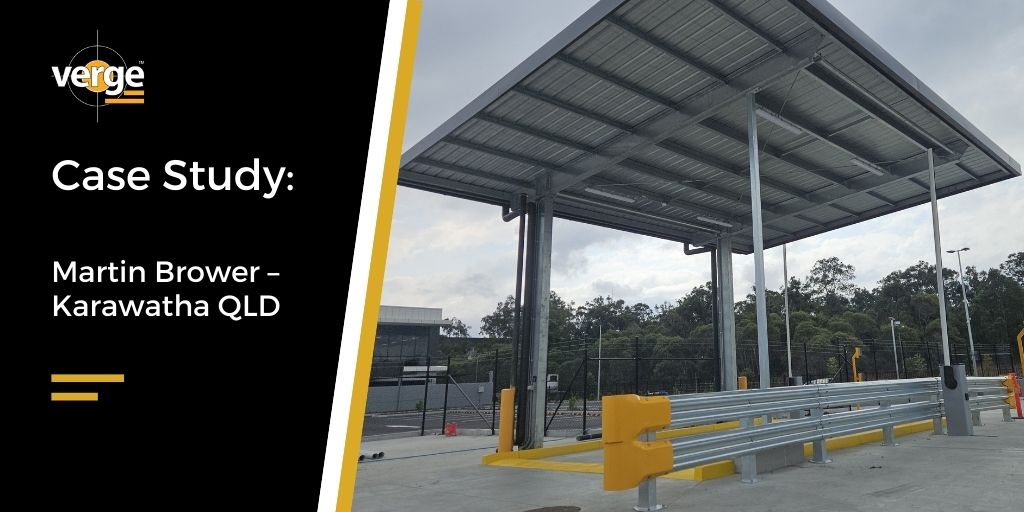
Martin Brower – Karawatha QLD

Martin Brower, a supply chain provider for fast food restaurants, needed to manage high volumes of vehicle, MHE and pedestrian traffic across their new Brisbane distribution centre. Verge partnered with Vaughan Constructions to supply and install a full safety barrier package. HD Barrier protected all internal pedestrian walkways, Double Guard-Pro provided asset protection at external boundaries and heavy vehicle areas, V-Gates managed pedestrian safety at all MHE crossover points, and steel overhead door protectors extended the lifespan of internal rapid doors.

WHY CHOOSE VERGE FOR MEAT PACKING SAFETY

Australian Made, Wash-Down Ready

Australian Made and Owned

Every Verge product is manufactured at our Glendenning, NSW facility, meaning faster delivery, local technical support, and products designed specifically for Australian conditions and WHS compliance requirements.

Built For Harsh, Wet, Cold Conditions

Meat processing facilities destroy safety infrastructure that is not built for the environment. Verge products are manufactured with finishes and materials suited to withstand washdown chemicals, constant moisture, and temperature variation, providing protection that lasts in conditions that punish lesser products.

WHS And Food Safety Compliant

Verge products are designed to meet Australian Work Health and Safety standards in a form that works within a food safety environment, helping meat processors document their hazard controls and satisfy both WHS and food safety auditors.

Minimises Production Downtime

Meat processing operates to tight schedules with limited windows for works. Our installation team works with facility managers to schedule and deliver installations during scheduled shutdowns and sanitation periods, minimising disruption to production.

Fast Lead Times

Local manufacturing means we can respond quickly when a safety gap needs to be addressed, without waiting on international supply chains or extended lead times.

PROTECT YOUR MEAT PACKING FACILITY WITH VERGE SAFETY BARRIERS

Every meat processing facility has a different layout, processing flow, and environmental challenge. Whether you need to separate forklifts from processing staff, protect a chiller entry, or secure a dispatch dock, Verge can help you find the right solution.

Contact us today for a free site assessment and quote.

$100 Verge gift voucher stack image

Receive A $100 Gift Voucher

SIGN UP TO OUR NEWSLETTER TO RECEIVE YOURS TODAY

*Applies to online orders only. *Cannot be used in conjunction with any other offer  **Must purchase within 3 months of receiving the voucher  ***Minimum order $1000

"*" indicates required fields

This field is for validation purposes and should be left unchanged.
Your Industry*

WAIT!

Before you go, check out this video.

If you need assistance with selecting a product, would like a quote or want to ask a question please call our friendly team on 1800 765 539

Download Brochure

  • This field is for validation purposes and should be left unchanged.